Pneumatic conveying system Manufacturers in Pune | SK Engineers

Pneumatic conveying system Manufacturers in Pune
whatsapp-now
enquire-now

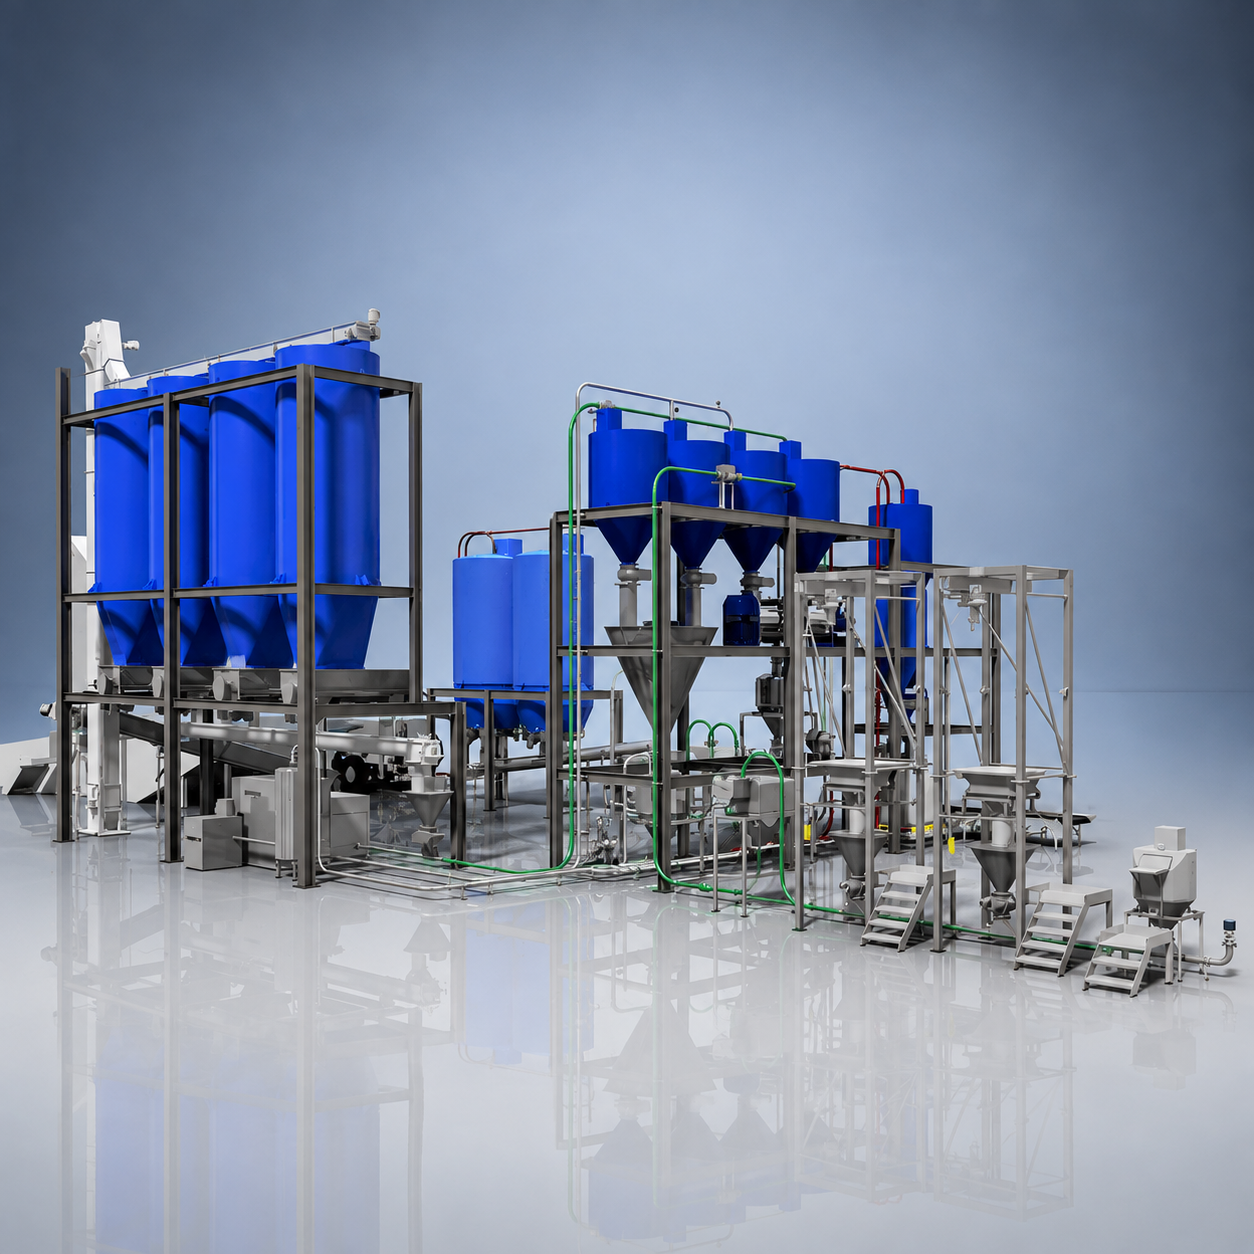
S k Engineers is leading Pneumatic Conveying System Manufacturers, Suppliers, Dealers and Exporters in Pune. A pneumatic conveying system is an advanced material handling solution designed to transport powders, granules, pellets, flakes, and bulk materials efficiently through enclosed pipelines using air pressure or vacuum. These systems are widely used in the food, pharmaceutical, chemical, plastics, cement, mineral, agriculture, and manufacturing industries for clean, safe, and dust-free material transfer. Unlike conventional mechanical conveyors, pneumatic conveying systems minimize material contamination, reduce product loss, and optimize plant layout by transporting materials over long distances with minimal manual handling.

Modern pneumatic conveying systems are equipped with blowers, vacuum pumps, rotary airlock valves, pipelines, cyclone separators, dust collectors, control panels, and automated feeding systems. Whether transferring flour, sugar, spices, plastic granules, cement, pharmaceutical powders, or chemical materials, these systems ensure reliable operation, high conveying efficiency, and improved workplace safety. Available in vacuum, pressure, dilute phase, and dense phase configurations, pneumatic conveying systems can be customized to suit different materials and production capacities.

What is a Pneumatic Conveying System?

A pneumatic conveying system is a material handling system that transports dry bulk materials through a closed pipeline using compressed air, vacuum, or a combination of both. The system eliminates the need for manual transportation and mechanical conveyors by moving materials efficiently from one processing stage to another while maintaining product quality and cleanliness.

A complete pneumatic conveying system typically includes a material feeding unit, rotary airlock valve, blower or vacuum pump, conveying pipeline, cyclone separator, dust collector, receiving hopper, and control panel. Depending on the material characteristics and production requirements, the system may operate using positive pressure, negative pressure, dilute phase, or dense phase conveying methods. These systems are suitable for handling powders, granules, pellets, flakes, grains, and other dry bulk materials in various industrial applications.

Working Principle of Pneumatic Conveying System

Step 1: Material Feeding

  • The bulk material is introduced into the conveying system through a hopper, screw feeder, rotary airlock valve, or automatic feeding unit.

Step 2: Air Generation

  • A blower, compressor, or vacuum pump generates the airflow required to transport the material through the pipeline.

Step 3: Material Conveying

  • The material is suspended within the airflow and conveyed through enclosed pipelines to the desired processing or storage location.

Step 4: Material Separation

  • At the receiving end, cyclone separators, filters, or dust collectors separate the conveyed material from the conveying air.

Step 5: Product Collection

  • The separated material is collected in storage hoppers, silos, processing equipment, or packaging systems for further production.

Types of Pneumatic Conveying System

As we are leading Pneumatic Conveying System Manufacturers in Pune, our Types are designed to meet different application requirements and industry standards, including the following types:

  • Vacuum Pneumatic Conveying System: Vacuum systems use negative pressure to gently transport powders and granules while minimizing dust generation and product contamination.
  • Pressure Pneumatic Conveying System: Pressure conveying systems use compressed air to move bulk materials over long distances with high conveying efficiency.
  • Dense Phase Pneumatic Conveying System: Dense phase conveying transports materials at low velocity and high pressure, making it suitable for fragile or abrasive materials.
  • Dilute Phase Pneumatic Conveying System: Dilute phase systems transport materials at higher air velocities and are commonly used for free-flowing powders and granules.
  • Pneumatic Powder Conveying System: Designed specifically for transferring powders such as flour, spices, chemicals, pigments, pharmaceutical ingredients, and minerals.
  • Granule Conveying System: These systems efficiently transport pellets, plastic granules, seeds, grains, and other free-flowing granular materials.
  • Food Grade Pneumatic Conveying System: Manufactured using food-grade stainless steel, these systems are suitable for hygienic handling of food powders and ingredients.
  • Pharmaceutical Pneumatic Conveying System: Designed for contamination-free pharmaceutical processing while complying with GMP and hygiene standards.
  • Chemical Pneumatic Conveying System: Suitable for safely transporting chemical powders, pigments, additives, and specialty materials in industrial environments.
  • Customized Pneumatic Conveying System: Engineered according to production capacity, material characteristics, conveying distance, and factory layout requirements.

Features of Pneumatic Conveying System

As Pneumatic Conveying System Suppliers in Pune, we have advanced features that ensure high precision, durability, and consistent performance.

Feature Description
Enclosed dust-free conveying Fully enclosed pipelines prevent dust emissions, product contamination, and material loss during transportation.
High conveying efficiency Optimized airflow and automated controls ensure fast, continuous, and reliable material transfer.
Flexible plant layout Pipelines can be routed horizontally, vertically, or around obstacles, reducing factory space requirements.
Automatic material handling Automated feeding and conveying minimize manual labor and improve production efficiency.
Low maintenance operation With fewer moving parts than mechanical conveyors, pneumatic systems require less maintenance and offer longer service life.
Energy-efficient design Advanced blowers, compressors, and control systems reduce power consumption while maintaining high conveying performance.

Benefits of Pneumatic Conveying System

As Pneumatic Conveying System Dealers in Pune, our products provide several benefits including consistent quality, smooth finish, and long service life.

  • Dust-Free Material Transfer: Enclosed conveying pipelines prevent airborne dust, creating a cleaner and safer production environment.
  • Reduced Product Contamination: Closed conveying systems protect materials from external contaminants, maintaining product purity and quality.
  • Improved Production Efficiency: Continuous automatic conveying reduces manual handling, increases productivity, and minimizes downtime.
  • Lower Operating Costs: Reduced labor requirements, low maintenance, and energy-efficient operation help decrease overall production costs.
  • Safe Material Handling: Automated conveying minimizes worker exposure to hazardous or dusty materials, improving workplace safety.
  • Versatile Industrial Applications: The system can handle powders, granules, pellets, flakes, grains, and bulk materials across multiple industries.

Applications of Pneumatic Conveying System

As Pneumatic Conveying System Exporters in Pune, our all types are used in various types of industrial sectors such as:

  • Food Processing Industry: Used for hygienically conveying flour, sugar, spices, starch, cocoa powder, milk powder, coffee, salt, and other food ingredients. It ensures contamination-free handling, minimal product loss, and efficient material transfer.
  • Pharmaceutical Industry: Transfers pharmaceutical powders, Active Pharmaceutical Ingredients (APIs), excipients, and tablet ingredients under contamination-free conditions. It maintains product purity and complies with strict pharmaceutical manufacturing standards.
  • Chemical Industry: Suitable for conveying chemical powders, pigments, additives, resins, carbon black, detergents, and specialty chemicals. It provides safe, dust-free, and efficient material handling throughout the production process.
  • Plastic Industry: Efficiently transports plastic granules, pellets, polymer powders, and masterbatch materials between processing equipment. It improves production efficiency while minimizing material waste and contamination.
  • Cement and Construction Industry: Used for conveying cement, fly ash, lime powder, silica, gypsum, and other construction materials. It ensures reliable bulk material handling with reduced dust generation and product loss.
  • Flour and Grain Processing: Transfers wheat flour, rice flour, maize flour, grains, pulses, and other food powders in milling and processing plants. It supports continuous production while maintaining product quality and hygiene.
  • Mineral Processing Industry: Handles minerals, industrial powders, fillers, and processed raw materials with minimal material loss. It offers efficient, dust-free conveying for consistent production performance.
  • Packaging and Manufacturing Plants: Automates the transfer of powders and bulk materials between processing equipment, storage silos, and packaging machines. It enhances workflow efficiency, reduces manual handling, and improves overall productivity.

Why Choose Us?

  • Advanced Material Handling Technology: We design high-performance pneumatic conveying systems that provide reliable, efficient, and dust-free material transportation.
  • Customized Engineering Solutions: Every conveying system is customized according to material characteristics, conveying distance, production capacity, and factory layout.
  • Premium Manufacturing Quality: Our systems are manufactured using high-quality components and durable materials for long-lasting industrial performance.
  • Complete Technical Support: We provide system design, installation, commissioning, operator training, maintenance assistance, and responsive after-sales service.
  • Cost-Effective and Energy-Efficient Solutions: Our pneumatic conveying systems deliver maximum productivity with low operating costs, helping businesses improve efficiency and profitability.

S k Engineers is leading Pneumatic Conveying System Manufacturers, Suppliers, Dealers and Exporters in Pune. A pneumatic conveying system is a reliable, efficient, and hygienic solution for transporting powders, granules, and bulk materials across various industries. With enclosed pipelines, automated material handling, energy-efficient operation, and flexible installation, these systems improve production efficiency while reducing contamination, dust emissions, and manual labor. Whether used in food processing, pharmaceuticals, chemicals, plastics, cement, or grain handling, investing in a modern pneumatic conveying system ensures consistent performance, lower operating costs, enhanced workplace safety, and long-term industrial productivity. Contact us Now!

FAQ’s

A pneumatic conveying system is a material handling solution that transports powders, granules, and bulk materials through enclosed pipelines using compressed air or vacuum.

The system can handle powders, granules, pellets, flakes, grains, flour, sugar, spices, chemicals, cement, plastic granules, pharmaceutical powders, and many other dry bulk materials.

Vacuum conveying uses negative pressure to pull materials through pipelines, while pressure conveying uses compressed air to push materials to the destination.

Dense phase conveying transports materials at lower velocities and higher pressure, making it suitable for fragile, abrasive, or easily damaged materials.

Dilute phase conveying moves materials at higher air velocities and is commonly used for free-flowing powders and granules.

Yes. Food-grade and pharmaceutical-grade pneumatic conveying systems are manufactured using hygienic stainless steel and comply with industry standards.
Location